Quality Control and Certificates at Radisson Impex
Quality control at Radisson Impex covers three things: how the steel is prepared, how the coating is applied, and how both are verified before handover.
Every job carries a test certificate and coating report, whether we coat at our Vasai plant or at your site.
What every job is measured against
-
ISO 9001:2015
Certified quality management system
-
Sa 2½
Blast-cleaning grade to ISO 8501-1 on every pipe
-
In-house
All testing carried out by our own team
-
Plant or site
The same certificate at Vasai or at your location
What our quality control covers
Preparation, application and verification are checked separately, and each one is recorded before the pipe leaves our hands.
-
How the steel is prepared
Every pipe is manually shot blasted to Sa 2½ before coating. New, used, rusted, black MS or GI pipe all follow the same preparation route.
-
How the coating is applied
Coating thickness and the testing regime are taken from the document your project is written to. Tighter figures in your specification override the standard.
-
How both are verified
Thickness, holiday, adhesion, impact and cure tests are run in-house and recorded on the coating report issued with every order.
Quality Begins Before the Coating Does
Surface preparation determines whether a coating bonds to the steel.
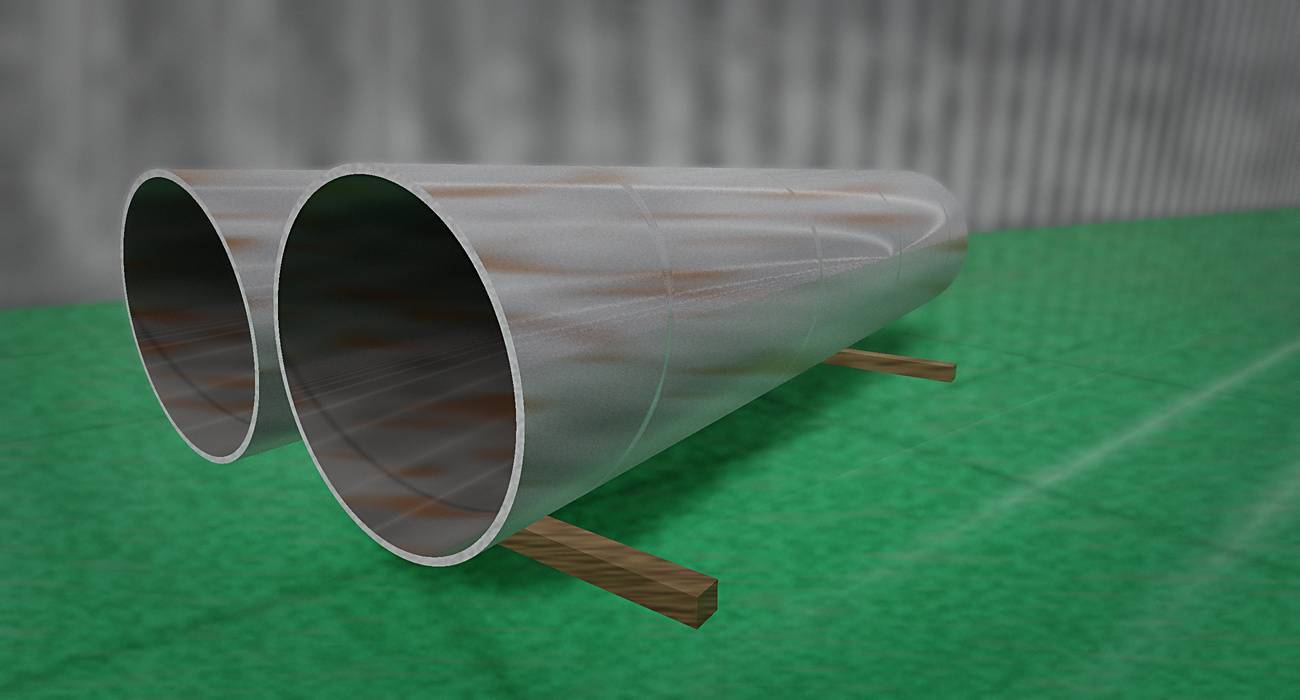
Every pipe is manually shot blasted to Sa 2½ before coating, the very thorough blast-cleaning grade defined in ISO 8501-1. New, used, rusted, black MS and GI pipe all follow the same preparation route.
-
Manual shot blasting on every pipe, checked against the ISO 8501-1 visual grade
-
Used and rusted pipe receives the same preparation before re-coating
-
GI pipe follows the same route as black MS pipe
Coating to Your Specification
Coating thickness and the testing regime are taken from the document your project is written to. Where your specification sets tighter thickness or test values than the standard it calls up, we coat to your figures.
| Standard | What it covers | Our service |
|---|---|---|
| ISO 21809-1:2018 | External three-layer polyolefin coatings (3LPE and 3LPP) for buried or submerged pipelines | 3LPE and 3LPP coating |
| ISO 21809-2:2026 | External single-layer fusion bonded epoxy coatings for pipelines | External FBE coating |
| IS 15659 (Part 1):2006 | Indian specification for three-layer PE and PP coatings | 3LPE and 3LPP coating |
| IS 15659 (Part 2):2006 | Indian specification for fusion bonded epoxy coatings | External FBE coating |
| AWWA C213-22 | Fusion bonded epoxy coatings and linings for steel water pipe and fittings | FBE on water lines |
| AWWA C210-24 | Liquid epoxy coatings and linings for steel water pipe and fittings | Liquid epoxy linings |
| API RP 5L2 and ISO 15741:2016 | Internal flow coatings for line pipe in non-corrosive gas service | Internal flow coating |
| AWWA C205-24 | Shop-applied cement mortar lining and coating for steel water pipe, 4 in (100 mm) and larger | Cement mortar lining |
| ISO 8501-1:2007 | Visual grades for blast-cleaned steel, including Sa 2½ | Surface preparation |
Your specification wins. If your project document calls for thicker build or stricter test values than the standard above, we coat and test to your figures.
What We Test
Each test below appears on the coating report issued with your order, run as applicable to the coating system.
| Test | What it checks | How we run it |
|---|---|---|
| Coating thickness | Build against the specified figure | Gauge readings along each pipe, in mm for 3LPE and 3LPP and in microns for epoxy |
| Holiday (spark) test | Pinholes and bare spots in the coating | High-voltage detector set to the voltage your specification names |
| Adhesion | Bond between coating and steel | Peel test on 3LPE and 3LPP, pull-off test on liquid epoxy |
| Impact | Resistance to handling damage | Falling-weight impact followed by a repeat holiday test, where your specification calls for it |
| Cure | Full cure of FBE and epoxy layers | Method named in your coating specification |
Independent Inspection and Records
Your third-party inspector can witness blasting, coating and testing, either at the Vasai plant or at a project site.
Inspections are hosted for the agency named in your purchase order.
Where your inspector can witness-
At the Vasai plant — every stage of shop coating and testing
-
At your project site — the same access when we coat onsite
-
Coating test certificate and coating report, issued for the job and covering every test run on the order
-
Datasheets for the coating materials used — manufacturer datasheets for every material applied
-
WRAS and FDA compliance documents, supplied by the paint manufacturer where food grade epoxy is specified
-
Coating warranty letter, issued with the order
Send Us Your Coating Specification
Share your pipe sizes, coating system and site location. Our technical team responds with a coating scope and a budgetary quote, together with the tests and documents your order will carry.